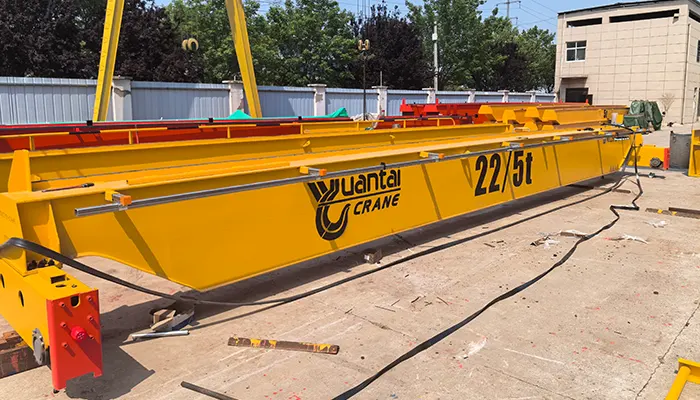
OEM Crane Quality Control in China: Buyer Inspection Guide
Content Quick Link
Quality Control for OEM Cranes from China: What Buyers Should Check
If you're sourcing overhead crane components, crane kits, or complete crane systems from China, product quality is probably at the top of your list. That's especially true for OEM orders—where the manufacturer builds equipment to your drawings, specs, and local assembly requirements.
The tricky part? You may not be able to visit the factory or watch every production stage yourself. So how do you make sure the steel is right, the welds hold up, the machined parts fit your existing equipment, and the electrical components match what was approved?
The answer is a solid quality control process backed by inspection records and testing evidence. Before you place an OEM order, agree on what gets inspected, when inspections happen, which standards and acceptance criteria apply, and what documents must be in hand before shipment.
This guide walks through the main quality control checkpoints for OEM cranes from China—incoming material inspection, welding, machining, component verification, assembly, functional testing, load testing, Factory Acceptance Testing (FAT), and third-party inspection.
Why Quality Control Matters When Sourcing OEM Cranes from China
When you buy standard crane products, you can compare models and specs from different suppliers. OEM manufacturing is a bit different. The factory may be producing crane components, crane kits, or complete equipment specifically for your business. The finished products must match your technical requirements and work with your existing designs or local assembly process.
A small mistake during manufacturing can cause big problems later. An incorrect wheel diameter might affect rail compatibility. A different motor model could change operating performance. And inaccurate mounting dimensions can make a crane kit a nightmare to assemble.
Some common quality risks include:
- Material mismatch: Steel grades, plate thicknesses, or material properties don't match the approved specs.
- Welding defects: Welds have visible defects or don't meet specified inspection requirements.
- Machining errors: Wheel dimensions, shaft diameters, bearing seats, or mounting holes fall outside required tolerances.
- Incorrect components: Motors, gearboxes, brakes, hoists, or electrical devices differ from the approved bill of materials.
- Assembly problems: Components don't fit correctly, alignment is off, or electrical connections are incomplete.
- Insufficient testing: Functional checks or specified load tests haven't been completed before shipment.
- Missing documentation: The supplier can't provide inspection reports, material certificates, or test records needed for project acceptance.
For crane importers and OEM buyers, these issues can lead to rework, delayed delivery, extra installation costs, and disputes with end customers. And for repeat orders, inconsistent manufacturing quality can damage your reputation in the local market.
That's why quality control needs to be discussed before production starts. Waiting until the finished crane is ready for shipment is too late to fix many manufacturing problems economically.
Set Quality Requirements Before Manufacturing Starts
Before a Chinese OEM crane manufacturer starts production, both sides should have a clear understanding of the approved design, component specs, inspection scope, and acceptance criteria.
Confirm the Approved Drawings and Technical Specifications
Drawings and technical specs are the reference documents for manufacturing and inspection. The factory shouldn't rely on informal discussions or outdated drawings when producing your crane components.
Depending on the order scope, approved technical documents may include:
- General arrangement (GA) drawings.
- Main girder, end carriage, trolley, and structural assembly drawings.
- Individual component and machining drawings.
- Mounting dimensions, connection details, and bolt-hole positions.
- Material grades and structural specifications.
- Hoist, motor, gearbox, brake, and electrical component specifications.
- Rated capacity, span, lifting height, speeds, and duty classification.
- Applicable design, manufacturing, and inspection standards.
For OEM crane kits, dimensional compatibility deserves particular attention. A set of end carriages or a trolley might meet its individual component specs but still fail to fit the buyer's existing crane structure if the wheelbase, mounting holes, or connection dimensions are wrong.
Prepare an Inspection and Test Plan (ITP)
An Inspection and Test Plan—commonly called an ITP—identifies the inspection activities required during manufacturing. It tells the factory and buyer what needs to be checked, at which production stage, and what records should be kept.
A typical OEM crane inspection plan may include the following stages:
| Inspection stage | What should be checked | Typical evidence |
|---|---|---|
| Incoming inspection | Steel materials, purchased components, models, specifications, and certificates | Incoming inspection reports, material certificates, component records |
| Welding inspection | Weld appearance, weld dimensions, and specified NDT requirements | Welding inspection and NDT reports |
| Machining inspection | Critical dimensions, tolerances, shaft seats, wheel profiles, and mounting interfaces | Dimensional inspection reports |
| Assembly inspection | Component installation, alignment, fasteners, wiring, and clearances | Assembly inspection records |
| Functional testing | Hoisting, lowering, travel, braking, controls, and safety devices | Functional test reports and videos |
| Load testing | Specified static or dynamic load test requirements, where applicable | Load test records |
| Final inspection | Product specifications, appearance, identification, accessories, and documentation | Final inspection report |
| Pre-shipment inspection | Quantity, packing, product identification, and shipping protection | Packing inspection records and photographs |
Not every OEM order needs the same inspection scope. A batch of machined wheels, for example, doesn't require the same FAT procedure as a complete overhead crane. The ITP should reflect the actual products, project requirements, and applicable standards.
Define Acceptance Criteria Before Production
It's not enough to write "inspect welding quality" or "check dimensions" in a purchase order. The factory needs to know what counts as an acceptable result.
Agree on the following points:
- Applicable dimensional tolerances and drawing revisions.
- Required material grades and certificates.
- Welding quality requirements and NDT scope.
- Approved component manufacturers, models, and technical ratings.
- Functional and load testing procedures.
- Inspection records and certificates required before shipment.
- How non-conforming products will be corrected and re-inspected.
For international OEM orders, these details should go into the technical agreement, purchase order, or approved ITP. This helps avoid disagreements when the products are ready for delivery.
Incoming Material and Component Inspection
Quality control starts when materials and purchased components arrive at the factory. Before cutting, welding, machining, or assembly begins, the manufacturer should check whether incoming items match the approved specs.
Steel and Raw Material Inspection
Steel plates, profiles, pipes, and other structural materials are used in overhead crane girders, end carriages, gantry structures, and supporting frames. Their grade, dimensions, and condition should be verified before production.
Buyers should check:
- Steel grade and material specification against the approved drawings.
- Plate thickness, profile dimensions, and material size.
- Surface condition—corrosion, cracks, deformation, and visible defects.
- Material certificates and heat numbers, where required.
- Material identification and traceability throughout production.
For projects requiring documented material verification, buyers may specify material certificates such as EN 10204 3.1. The required certificate type should be agreed in the purchase specification rather than assumed for every order.
Technical reference for steel grades: For crane structures, common Chinese steel grades include Q235B (equivalent to ASTM A36 in yield strength) and Q355B (higher strength, comparable to S355). Buyers should specify not just the grade but also the impact toughness requirement—Charpy V-notch at 0°C or -20°C, for example—if the crane will operate in cold environments. The steel certificate should include chemical composition and mechanical properties tested per the applicable standard.
Purchased Crane Component Inspection
Many OEM crane manufacturers purchase certain components from specialist suppliers. These may include electric hoists, motors, gearboxes, brakes, bearings, wire ropes, electrical devices, and safety equipment.
The factory should verify the actual products against the approved component list, not just the supplier's quotation or purchase record.
| Component | Key points to verify |
|---|---|
| Electric hoist or winch | Rated capacity, lifting height, lifting speed, model, motor rating, duty class |
| Motor | Manufacturer, model, power, speed, voltage, frequency, insulation and protection ratings |
| Gearbox | Model, transmission ratio, rated torque, mounting dimensions, and output shaft |
| Brake | Brake type, rated braking torque, operating voltage, and compatibility |
| Wheels and bearings | Dimensions, material, bearing type, load rating, and mounting details |
| Electrical panel and controls | Voltage, frequency, control method, electrical components, and protection rating |
| Safety devices | Overload protection, limit switches, emergency stop, and other specified devices |
| Wire rope and hook | Diameter, construction, rated capacity, identification, and applicable certificates |
One point worth checking carefully is the component nameplate. A motor may look almost identical to the approved model, but its power, speed, voltage, or duty rating could be different. The same applies to hoists, brakes, and gearboxes.
Motor verification data points: For crane duty motors, buyers should confirm the duty classification—S3 intermittent duty with a specified cyclic duration factor, or S4 with equivalent starting cycles. Insulation class should be at least Class F for crane applications, with temperature rise limited to Class B. For motors rated above 30 kW, space heaters are recommended to prevent condensation during standby. Verification should include locked-rotor current and torque values against the nameplate to confirm the motor matches the approved spec.
Material Certificates and Component Records
Depending on the order, buyers may request:
- Steel material certificates and heat number records.
- Component datasheets and manufacturer documentation.
- Incoming material and component inspection reports.
- Motor, gearbox, hoist, and electrical component nameplate photographs.
- Batch numbers or serial number records for traceability.
For an OEM buyer, these documents make it easier to confirm that the manufacturer used the agreed materials and components. They're also useful when your own customer requests technical documentation after delivery.
Welding Quality Inspection
Welding quality is a big deal in crane manufacturing, especially for load-bearing structures like main girders, end carriages, gantry frames, and other welded assemblies. A proper welding inspection should cover more than the final appearance of the weld. The inspection scope may include welding procedures, welder qualifications, visual inspection, and non-destructive testing (NDT), depending on the design and project requirements.
Visual Welding Inspection
Visual testing is usually the first step in checking welded joints. The inspector examines the weld surface and compares weld dimensions and location with the approved drawings and welding requirements.
Typical checks include:
- Weld length, size, and position.
- Weld continuity and surface finish.
- Visible cracks, undercut, porosity, overlap, and incomplete filling.
- Joint preparation and fit-up, where accessible.
- Removal of spatter and other surface imperfections where required.
Visual inspection can catch many surface problems, but it can't confirm the absence of internal weld defects. That's why additional NDT may be required for specified joints.
Welding Procedures and Welder Qualifications
For projects with defined welding quality requirements, buyers should ask whether the manufacturer has suitable welding procedures and qualified personnel.
Relevant records may include:
- Welding Procedure Specification (WPS).
- Procedure Qualification Record (PQR), where required.
- Welder qualification records.
- Welding consumable control records.
- Welding inspection records.
The exact documentation depends on the applicable welding standard, project specification, and contract requirements.
Non-Destructive Testing (NDT)
Non-destructive testing examines welds or materials without damaging the finished component. The appropriate method depends on the material, joint configuration, defect type, and inspection requirements.
| NDT method | What it detects | Typical application |
|---|---|---|
| VT – Visual Testing | Visible surface imperfections | General weld inspection |
| MT – Magnetic Particle Testing | Surface and near-surface discontinuities | Suitable ferromagnetic materials and welds |
| PT – Penetrant Testing | Surface-breaking defects | Suitable non-porous materials |
| UT – Ultrasonic Testing | Internal discontinuities | Specified welds and structural joints |
| RT – Radiographic Testing | Internal weld discontinuities | Selected welds where radiographic examination is specified |
Not every weld needs all these inspection methods. The required NDT method, inspection percentage, acceptance criteria, and reporting format should be specified in the ITP or project documents.
Welding acceptance criteria by quality level: When specifying welding quality, buyers should reference ISO 5817 quality levels B, C, or D. For crane load-bearing structures subject to dynamic or fatigue loading, Level B (stringent) is typically appropriate. For general structural welds under static loading, Level C (intermediate) may suffice. Key acceptance limits for Level B include continuous undercut ≤ 0.05t (max 0.5 mm), angular misalignment ≤ 1°, and linear misalignment ≤ 0.05t (max 2 mm). Cracks, lack of fusion, and incomplete root penetration are not permitted at any quality level. Buyers should specify the required quality level in the ITP rather than leaving it to the manufacturer's discretion.
NDT acceptance standards: For UT of full-penetration ferritic steel welds (8–100 mm thickness), acceptance levels should align with ISO 11666. Acceptance level 2 corresponds to ISO 5817 quality level B, and level 3 corresponds to quality level C. This correlation helps buyers verify that the NDT acceptance criteria match the specified weld quality level.
What should buyers request? Ask for the welding inspection records and NDT reports for the joints identified in the inspection plan. A general statement that the factory performs NDT doesn't tell you which welds were examined or what the results were.
Machining and Dimensional Inspection
Machining accuracy is especially important for OEM crane components. A wheel, shaft, bearing seat, or mounting plate may be manufactured from the correct material but still cause problems if its dimensions are off. This matters even more when you're buying crane components from China for local assembly. The parts must fit the existing structure and interface dimensions without unnecessary modification.
Machined Component Inspection
Depending on the product, key machining dimensions may include:
- Crane wheel diameter and tread profile.
- Shaft diameter and bearing mounting positions.
- Gearbox and motor mounting dimensions.
- Coupling dimensions and connection details.
- Bolt-hole positions and center distances.
- Keyways, grooves, and other machined features.
Structural and Assembly Dimensions
For complete cranes and structural assemblies, buyers may also need to verify:
- Main girder length and relevant span dimensions.
- End carriage length and wheelbase.
- Wheel alignment and parallelism.
- Mounting interfaces and connection dimensions.
- Hoist or trolley mounting positions.
- Hole spacing and structural connection locations.
For a replacement end carriage or OEM crane kit, don't check only the overall length. Wheelbase, wheel diameter, rail compatibility, mounting hole positions, and the connection to the main girder all need to match the approved drawings.
Critical wheel and rail interface data: Crane wheel tread profile should match the rail type (e.g., QU70, QU80, or A-series rails). Wheel diameter tolerance typically falls within h9 or h8 depending on the application. For wheels used in pairs, the diameter difference between left and right wheels on the same end carriage should not exceed 0.5 mm to prevent skewing and uneven rail wear. Buyers should request measured values for wheel diameter, tread hardness (typically 300–380 HB for forged wheels), and wheelbase distance—not just a pass/fail statement.
Dimensional Inspection Tools and Reports
Common inspection equipment includes calipers, micrometers, height gauges, dial indicators, laser measurement equipment, and coordinate measuring machines (CMM), where appropriate.
Buyers should ask for dimensional inspection reports showing the measured values for important dimensions, the specified tolerances, and whether the results pass inspection. A report that simply says "OK" provides much less useful information.
Component Verification Before Assembly
Before assembly begins, the factory should confirm that the correct components have been selected and supplied for the order. This is an important checkpoint for OEM crane manufacturers and importers because component substitutions can affect compatibility, performance, and maintenance.
Compare the actual components with the approved bill of materials (BOM), drawings, and technical datasheets.
| Component or system | What buyers should verify |
|---|---|
| Hoist or winch | Capacity, lifting height, lifting speed, model, motor rating, and duty class |
| Motor and gearbox | Power, speed, transmission ratio, mounting dimensions, and operating duty |
| Brake | Type, braking torque, operating voltage, and installation arrangement |
| Wheels and end carriages | Wheel diameter, material, wheelbase, bearing arrangement, and mounting dimensions |
| Electrical system | Voltage, frequency, control method, wiring arrangement, and protection rating |
| Safety devices | Limit switches, overload protection, emergency stop, and specified interlocks |
| Wire rope and hook | Diameter, construction, rated capacity, hook type, and identification |
If a manufacturer needs to substitute a component because the original model is unavailable, the change should be submitted for buyer approval before installation. The replacement must meet the required technical and dimensional specs.
This is particularly important for distributors and crane manufacturers who sell equipment under their own brand. An unapproved change can create compatibility problems and make future spare parts procurement difficult.
Brake verification data: For hoisting brakes, buyers should verify the rated braking torque against the required holding torque. The brake should be rated for the duty class of the crane (e.g., M5, M6 per FEM or H2, H3 per ISO). For thruster brakes, the thruster voltage and frequency must match the site power supply. The brake should include a manual release mechanism for emergency lowering.
Assembly Inspection: Check How the Components Fit Together
Once components have passed incoming inspection and verification, the next step is assembly. At this stage, the factory should check whether the mechanical and electrical parts have been installed correctly and whether the complete assembly follows the approved drawings.
Mechanical Assembly Inspection
Typical mechanical checks include:
- Hoist and trolley installation positions.
- Motor and gearbox alignment.
- Brake installation and adjustment.
- Wheel and bearing installation.
- Coupling and shaft connections.
- Fastener installation and tightening.
- Lubrication of specified moving parts.
- Clearances and possible mechanical interference.
Alignment tolerances to request: For motor-gearbox coupling alignment, angular misalignment should typically not exceed 0.1 mm per 100 mm of coupling length, and parallel misalignment should be within 0.05–0.1 mm depending on coupling type. For brake installation, the brake drum runout should be within 0.1 mm to prevent vibration and uneven wear. These measured values should appear in the assembly inspection record.
Electrical Assembly Inspection
For the electrical system, the inspector should compare the actual wiring and installation with the approved electrical drawings.
Check:
- Control panel installation and component arrangement.
- Wiring connections and terminal identification.
- Cable routing, support, and protection.
- Grounding and electrical protection.
- Motor connections and rotation direction.
- Limit switches and safety circuit connections.
- Remote control or pendant control operation.
Electrical verification data: Insulation resistance testing should be performed on all power circuits, with a minimum acceptable value of 1 MΩ at 500 V DC (or per the applicable standard). Grounding continuity resistance should be measured and documented—typically required to be below 0.1 Ω. For control circuits, the functional test should verify that all safety interlocks (emergency stop, limit switches, overload) operate correctly and that the control voltage is within the specified range.
Assembly Fit, Finish, and Identification
The final assembly inspection should also cover physical condition and product identification.
- Check that the assembled components match the approved drawings.
- Look for interference between moving and stationary parts.
- Check structural connections and visible fasteners.
- Inspect paint coverage and surface protection.
- Confirm that warning labels, nameplates, and identification marks are installed.
A component can pass its individual inspection and still cause a problem after installation. Assembly inspection is where the factory checks whether the complete system fits and works as intended.
Functional Testing and Crane Load Testing
Before an OEM crane or crane kit is released for shipment, the factory should carry out the functional checks required by the agreed inspection plan. For complete overhead cranes, these checks normally cover lifting, trolley travel, crane travel, braking, control, and safety functions.
No-Load Functional Testing
No-load testing checks whether the crane's mechanisms and electrical systems operate correctly without a suspended test load.
Depending on the crane design, the inspection may cover:
- Hoisting and lowering operation.
- Trolley cross travel.
- Crane long travel.
- Motor rotation and operating direction.
- Brake response and stopping performance.
- Upper and lower limit switch operation.
- Emergency stop function.
- Pendant or radio remote control operation.
- Abnormal noise, vibration, or overheating.
Measurable functional criteria: Hoisting and lowering speeds should be measured and compared with the rated speed (typically within ±5% tolerance). Brake stopping distance under no load should be recorded. Travel speeds for trolley and bridge should be verified. For variable-frequency drives, acceleration and deceleration times should match the programmed parameters. Any abnormal vibration or noise should be documented with location and severity.
Static and Dynamic Load Testing
Load testing checks the crane's performance under specified loading conditions. The test procedure and acceptance criteria should follow the applicable crane standard and project specification.
Two commonly discussed types are:
- Static load test: The crane is subjected to a specified stationary test load to check structural and mechanical behavior under the defined test conditions.
- Dynamic load test: The crane operates with a specified test load to check the performance of lifting, travel, braking, and other relevant mechanisms.
Load test values per ISO 4310: Under ISO 4310, the static test load is typically 125% of rated capacity, applied and held for a specified duration (commonly 10 minutes) to check for permanent deformation. The dynamic test load is typically 110% of rated capacity, with the crane operated through multiple cycles (at least three lift/lower cycles) to verify brake and mechanism performance. Buyers should confirm the applicable standard and any project-specific requirements, as some contracts may specify different percentages or additional tests.
The test load, test sequence, duration, measurement requirements, and acceptance criteria should be confirmed before testing. There's no single overload percentage or test procedure that should be assumed to apply to every crane and every project.
What to measure during load testing: During static testing, the inspector should measure and record any permanent deflection of the main girder after the load is removed. For dynamic testing, brake stopping distance under load, any abnormal noise from gearboxes or bearings, and motor current draw during lifting should be recorded. These values provide a baseline for comparison with future inspections and help verify that the crane will perform as expected in service.
What Should Be Recorded During Crane Testing?
Buyers should request a test report that identifies the equipment and records the actual results.
| Test record | Information to include |
|---|---|
| Equipment identification | Crane or component model, serial number, and rated capacity |
| Test information | Test date, location, test method, and applicable procedure |
| Test load | Actual test load and relevant loading conditions |
| Operating results | Hoisting, travel, braking, and other specified functions |
| Inspection findings | Observed defects, abnormal behavior, or deviations |
| Corrective actions | Repairs, adjustments, and re-test results, where applicable |
| Final acceptance | Pass/fail result and authorized inspection approval |
For buyers who can't attend the factory test, a signed test report supported by photographs or videos provides useful evidence. For critical projects, an independent inspector may also witness the specified tests.
Factory Acceptance Test (FAT): What Should Buyers Check?
A Factory Acceptance Test (FAT) is a planned inspection and testing activity carried out before the equipment is released from the factory. It gives the buyer an opportunity to verify that the finished product meets the agreed technical requirements. For OEM crane manufacturing, the FAT scope depends on whether you're purchasing individual components, a crane kit, or a complete crane system.
What Is Included in a Crane FAT?
A typical FAT for a complete overhead crane may include:
- Verification against approved GA and component drawings.
- Checking component models, nameplates, and specifications.
- Dimensional inspection of critical parts and assemblies.
- Mechanical and electrical assembly checks.
- No-load functional testing.
- Safety device and control system checks.
- Static or dynamic load testing, where specified and applicable.
- Review of inspection reports and test documentation.
For a batch of crane wheels, end carriages, or hoist components, the FAT may focus more on dimensional inspection, material verification, component identification, and functional checks relevant to the products supplied.
Can Buyers Attend the FAT Remotely?
Yes. Overseas buyers don't always need to travel to China to follow every inspection activity. Remote inspection can be arranged for suitable checks, provided the factory has the equipment and communication facilities to support it.
Practical options include:
- Live video inspection of the finished products.
- Live viewing of nameplates, serial numbers, and component models.
- Recorded videos of functional testing.
- Sharing dimensional inspection reports and test results.
- Video review of packing and product identification before shipment.
Remote FAT is useful for checking visible details and reviewing documents. It doesn't replace physical measurement, specialized NDT, or independent inspection where those activities are required by the contract.
FAT Acceptance and Outstanding Issues
Before the FAT, prepare a checklist based on the approved drawings and inspection plan. During the inspection, record any defects or items that don't meet the agreed requirements.
For each outstanding issue, agree on:
- What needs to be corrected.
- Who is responsible for the corrective action.
- When the correction must be completed.
- Whether a re-inspection or re-test is required.
- What evidence is needed before final acceptance.
Don't treat a verbal promise to correct an issue as final acceptance. Keep the findings and corrective actions in the FAT report or an agreed inspection record.
Third-Party Inspection for OEM Cranes in China
For overseas buyers, third-party inspection is one way to get independent verification of manufacturing quality before shipment. It's particularly useful when the buyer can't send its own quality engineer to the factory.
When Should Buyers Arrange Third-Party Inspection?
Independent inspection is worth considering in the following situations:
- You're placing your first order with a new Chinese OEM crane manufacturer.
- The order has a high value or involves technically complex equipment.
- The crane will operate in demanding industrial conditions.
- Your end customer or EPC contractor requires independent inspection.
- You need to verify product consistency across repeat OEM orders.
- The contract specifies witnessed testing or independent acceptance.
What Can a Third-Party Inspector Check?
The inspection scope can be arranged according to the product and contract requirements.
| Inspection activity | Typical verification |
|---|---|
| Material inspection | Material grade, dimensions, certificates, and traceability |
| Component inspection | Models, nameplates, ratings, brands, and quantities |
| Welding inspection | Weld appearance, dimensions, and specified NDT records |
| Dimensional inspection | Critical component and assembly dimensions |
| Assembly inspection | Mechanical fit, alignment, electrical installation, and finish |
| Functional testing | Specified operating functions and safety devices |
| Load test witnessing | Specified test procedure, load, and test results |
| Pre-shipment inspection | Product quantity, identification, packing, and shipping condition |
Which Third-Party Inspection Companies Can Buyers Use?
International inspection and testing organizations such as SGS, TÜV, Bureau Veritas, and Intertek may provide inspection services in China, depending on the location, product, and requested scope.
Buyers can also appoint another qualified independent inspection agency that meets the project's requirements. Before booking, confirm that the inspector has the technical experience and authorization needed for the specific inspection activities—especially welding inspection, NDT, and load testing.
What Should the Third-Party Inspection Agreement Specify?
To avoid confusion, the buyer should define the following before the inspector visits the factory:
- Products and quantities to be inspected.
- Inspection stages and factory notification requirements.
- Applicable standards and acceptance criteria.
- Sampling requirements, if applicable.
- Tests to be witnessed and documents to be reviewed.
- Required photographs and inspection reports.
- Procedure for handling rejected items and re-inspection.
Keep in mind that third-party inspection doesn't automatically guarantee product quality. The inspector can only verify the items and activities included in the agreed inspection scope.
Inspection Reports and Documents to Request Before Shipment
Inspection records are the evidence that manufacturing and testing activities have been completed. For an OEM buyer, they also help connect the approved drawings and specifications with the actual products delivered.
Before shipment, ask the manufacturer to provide the documents required by your purchase contract and ITP.
| Document or record | What it helps verify |
|---|---|
| Approved GA and component drawings | Product configuration, dimensions, and manufacturing reference |
| Material certificates | Material grade and traceability |
| Incoming inspection reports | Raw materials and purchased components were checked |
| Welding inspection reports | Specified welded joints were inspected |
| NDT reports | Specified non-destructive tests and results |
| Dimensional inspection reports | Measured dimensions against drawing tolerances |
| Component datasheets and nameplate records | Actual components match approved specifications |
| Assembly inspection reports | Mechanical and electrical assembly checks |
| Functional test reports | Specified operating functions were tested |
| Load test reports | Specified load test procedure and results, where applicable |
| FAT report | Final factory inspection findings and acceptance status |
| Third-party inspection report | Independent inspection findings, if arranged |
| Packing list and identification records | Shipment quantities, product identification, and packing details |
Not every document is necessary for every order. A small batch of standard crane components, for example, may not require the same documentation package as a complete heavy-duty overhead crane. The important thing is to agree on the required records before production and include them in the order documents.
OEM Crane Quality Control Checklist for Buyers
If you're importing crane components or complete cranes from China, the following checklist can help your purchasing and quality teams organize inspections. It can also be used when comparing the quality control capabilities of different OEM crane manufacturers.
| Production stage | Buyer checklist | Evidence to request |
|---|---|---|
| Before production | Confirm approved drawings, specifications, BOM, and ITP | Approved technical documents |
| Raw materials | Check material grades, dimensions, condition, and traceability | Material certificates and incoming inspection records |
| Purchased components | Verify brands, models, ratings, nameplates, and quantities | Datasheets, nameplate photographs, component inspection records |
| Welding | Check weld appearance and specified welding requirements | Welding inspection and NDT reports, where required |
| Machining | Measure critical dimensions and tolerances | Dimensional inspection reports |
| Assembly | Check installation, alignment, connections, wiring, and safety devices | Assembly inspection records and photographs |
| Functional testing | Test hoisting, travel, braking, controls, and limit switches | Functional test reports or videos |
| Load testing | Verify the agreed test method, load, and results | Load test report, where applicable |
| FAT | Review final inspection findings and close outstanding issues | FAT report and acceptance records |
| Documentation | Confirm all contractually required reports and certificates are available | Final quality documentation package |
| Before shipment | Check quantities, identification, packing, and transport protection | Packing inspection records and photographs |
Practical tip: If you're ordering OEM crane components repeatedly, keep the approved drawings, BOM, inspection criteria, and previous inspection reports as controlled reference documents. This makes it easier to compare production batches and identify changes before they become recurring problems.
Common Quality Control Problems and How Buyers Can Prevent Them
Many manufacturing problems can be avoided if the buyer and supplier agree on technical details before production. The table below covers some issues commonly worth checking when sourcing OEM crane products.
| Potential problem | Possible consequence | How buyers can prevent it |
|---|---|---|
| Steel grade does not match the specification | Material performance may not meet the design requirements | Specify material grades and request certificates and traceability records |
| Motor or gearbox model is incorrect | Operating performance or installation may be affected | Check component nameplates and datasheets against the approved BOM |
| Poor welding quality | Structural defects, rework, or delayed acceptance | Define welding inspection requirements and NDT scope in the ITP |
| Machining dimensions are incorrect | Components may not fit during assembly | Identify critical dimensions and request measured inspection reports |
| Unapproved component substitution | Compatibility, performance, or spare parts problems | Require written approval before changing any specified component |
| Incomplete functional testing | Operating faults may appear after delivery or installation | Agree on the functional test procedure and FAT requirements |
| Missing inspection documents | Project acceptance and traceability may become difficult | List required quality documents in the purchase contract |
| Insufficient packing protection | Components may be damaged during international transport | Specify export packing and arrange pre-shipment inspection |
How to Evaluate the Quality Control Capability of a Chinese OEM Crane Manufacturer
Before choosing a Chinese crane manufacturer for OEM production, look beyond the quotation and delivery time. A competitive price matters, of course, but the supplier must also be able to manufacture consistently and provide the inspection evidence your business needs.
Here are some practical questions to ask during supplier evaluation:
- Does the factory have a documented quality management system?
- Can it provide material certificates and component traceability records?
- Does it have in-house welding and machining inspection capabilities?
- Can it provide qualified welding and NDT inspection records where required?
- Are critical dimensions checked against approved drawings?
- Can it verify motors, hoists, gearboxes, brakes, and electrical components before assembly?
- Does it carry out functional testing and specified load testing before shipment?
- Can it prepare an ITP and FAT procedure for overseas buyers?
- Can buyers arrange remote inspection or appoint a third-party inspection company?
- Can the factory maintain consistent specifications and quality across repeat OEM orders?
- How are non-conforming products handled, corrected, and re-inspected?
Does ISO 9001 Certification Guarantee Crane Product Quality?
ISO 9001 certification is useful when evaluating a manufacturer's quality management system. It indicates that the organization has a quality management framework covering areas such as process control, documentation, and continual improvement.
But it doesn't prove that every crane or component produced by the factory meets your technical specifications. Product-level quality still needs to be verified through material inspection, dimensional checks, component verification, functional testing, and other inspections required by the project.
When comparing OEM crane suppliers in China, consider both the manufacturer's quality management system and its ability to provide actual inspection and test records for your order. Check crane certifications of Yuantai Cranes.
FAQs About OEM Crane Quality Control
Below are the most common questions buyers ask about inspecting and verifying OEM crane quality before shipment, covering pre-shipment checks, factory inspections, required documents, load testing, FAT, third-party inspection, and ISO 9001 certification.
How do I inspect overhead crane components before shipment?
Start by comparing the actual components with the approved drawings, BOM, and technical specifications. Check nameplates, models, ratings, dimensions, material records, and visible condition. For important components, request inspection reports and datasheets. If you can't visit the factory, arrange remote inspection or appoint a third-party inspector.
What should I check during a crane factory inspection in China?
Check the main production stages: incoming materials, purchased components, welding, machining, assembly, functional testing, and final packing. For complete cranes, also review the specified load test and FAT records. The inspection scope should be agreed in advance through an ITP.
What documents should an OEM crane manufacturer provide?
Depending on the order, documents may include approved drawings, material certificates, incoming inspection reports, welding and NDT reports, dimensional inspection reports, component datasheets, assembly inspection records, functional test reports, load test records, FAT reports, and packing lists.
Is a load test required for every overhead crane?
Load testing requirements depend on the applicable standards, project specification, crane type, and contract. Buyers should confirm the required test method, test load, acceptance criteria, and witnessing arrangements before production. Don't assume the same load test procedure applies to every crane.
What is the difference between a crane FAT and a load test?
A load test checks crane performance under specified loading conditions. A Factory Acceptance Test is a broader inspection and testing process that may include drawing verification, component checks, dimensional inspection, functional testing, safety device checks, load testing, and document review. A load test may be one part of the FAT.
Can I arrange third-party inspection at a Chinese crane factory?
Yes. Buyers can appoint an independent inspection company to check materials, components, welding, dimensions, assembly, testing, and packing according to the agreed inspection scope. Confirm the inspector's technical qualifications and the inspection criteria before the factory visit.
Can a buyer inspect an OEM crane remotely before shipment?
Yes, for suitable inspection activities. The factory can arrange live video calls, recorded functional tests, nameplate verification, document reviews, and packing videos. Remote inspection is useful for overseas buyers, although physical measurement, NDT, and independent witnessing may still be needed for certain requirements.
What is included in a quality control checklist for imported cranes?
A practical checklist should cover approved drawings, materials, components, welding, machining, assembly, functional testing, load testing where applicable, FAT, inspection documentation, and pre-shipment packing. The exact items depend on whether you're importing individual components, a crane kit, or a complete crane.
How can I verify that crane components match approved drawings?
Use the latest approved drawing revision and BOM as inspection references. Check key dimensions with suitable measuring tools, compare component nameplates and model numbers with the specifications, and request dimensional inspection reports for critical interfaces. Record and approve any proposed changes before production or assembly.
Does ISO 9001 certification guarantee crane product quality?
No. ISO 9001 relates to the manufacturer's quality management system. It doesn't replace inspection of the actual product. Buyers should still check technical specifications, manufacturing quality, component records, testing results, and contractually required inspection reports.
Work with a Chinese OEM Crane Manufacturer That Supports Quality Inspection
Choosing an OEM crane manufacturing partner involves more than comparing prices. You need a supplier that can understand your drawings, follow the agreed technical specifications, verify purchased components, control manufacturing dimensions, and provide the inspection records required by your business.
Yuantai Crane supports OEM manufacturing for overseas crane companies, distributors, importers, and industrial project buyers. Depending on the order scope, products can include crane components, end carriages, hoists, crane kits, and complete overhead or gantry crane systems.
For OEM projects, the inspection and testing scope can be discussed according to the approved drawings, technical requirements, and project documentation. This may include:
- Incoming material and purchased component verification.
- Welding and dimensional inspection.
- Mechanical and electrical assembly checks.
- Functional testing and load testing where applicable.
- Factory acceptance testing and inspection documentation.
- Coordination with third-party inspection agencies when required.
Whether you're sourcing crane components for local assembly or looking for a Chinese OEM manufacturer for complete crane systems, it's worth discussing quality requirements before production begins.
Planning an OEM crane order from China? Send us your drawings, BOM, existing crane specifications, or project requirements. Our engineering team can review the technical details and discuss the manufacturing scope, inspection checkpoints, testing requirements, and quality documents needed for your order.
Related Articles
Reference articles for overseas crane companies evaluating Chinese OEM manufacturing, covering cooperation models, kit vs. local manufacturing decisions, brand building, sourceable products, supplier selection, technical requirements, quality control, and order pricing.
Focus: Explain OEM manufacturing, how overseas companies cooperate with Chinese crane factories, what can be manufactured, and how the cooperation works.
Why it matters: Buyers need to understand whether they can use a Chinese factory as a manufacturing partner without building their own production facilities or giving up their local market and brand.
Target buyers: Local crane manufacturers, crane engineering companies, established crane distributors, and companies planning to launch their own crane product range.
Focus: Compare three business models: local manufacturing, importing complete cranes, and importing crane kits or major components for local assembly.
Why it matters: This is a practical investment decision. Buyers want to know which parts they should manufacture themselves and which parts are more suitable to source from China.
Focus: Private-label manufacturing, customer branding, nameplates, drawings, product specifications, packaging, warranty, and division of responsibilities.
Why it matters: Buyers may have their own customers and sales channels but lack the manufacturing capacity to produce every crane or component themselves. They need to know whether they can sell products under their own brand.
Focus: Explain the products buyers can source: end carriages, hoists, trolleys, travel mechanisms, wheels, motors, brakes, electrical systems, crane kits, and complete overhead and gantry cranes.
Why it matters: Many buyers know they want to source from China but are unsure how much of the crane manufacturing process they can outsource. This article helps them identify the products relevant to their business.
Focus: Factory capability, engineering team, manufacturing processes, welding and machining, assembly, testing, export experience, and supplier verification.
Why it matters: Overseas buyers face difficulty distinguishing a real manufacturer from a trading company or a supplier that outsources most of the work. They need evidence of manufacturing and engineering capability.
Focus: What buyers need to provide before production: GA drawings, capacity, span, lifting height, duty class, wheel loads, connection dimensions, motors, electrical requirements, operating environment, and applicable standards.
Why it matters: Incomplete specifications cause quotation delays, design changes, component mismatches, and problems during local assembly. This article helps buyers prepare a useful technical inquiry.
Focus: Incoming material inspection, welding, machining, component verification, assembly, functional testing, load testing where applicable, FAT, inspection reports, and third-party inspection.
Why it matters: The buyer may not be present during manufacturing. They need to know what evidence to request and how to check that the delivered products match the approved drawings and specifications.
Focus: How OEM prices are calculated, customization costs, minimum order quantities, sample orders, production lead times, export packaging, freight, Incoterms, payment terms, and warranty.
Why it matters: Buyers need to calculate the total purchasing cost, not just the factory quotation. They also need to understand whether their order volume and delivery requirements are practical.
Article by Bella ,who has been in the hoist and crane field since 2016. Bella provides overhead crane & gantry crane consultation services for clients who need a customized overhead travelling crane solution.Contact her to get free consultation.
Yuantai Cranes
Overhead Crane Manufacturer with CE, ISO, SGS, CNEX Certificates.
- Main Specifications - Capacity: 0.5–550 tons | Span: up to 40m | Speed: 0.8–12 m/min | Duty: A3–A7 | Power: 380–690V, 50/60Hz | Control: pendant/remote/cabin
- Full engineering: FEA/PLC/VFD + in-house build + global delivery + on-site support, for workshops, factories, EPC contractors, industrial projects, etc.
- Support: design, manufacturing, testing, service – end-to-end, customized lifting solutions worldwide.
How to Get an Accurate Crane Price for Your Application?
Tips: Copy the spec list, fill in your details, and paste it into the form on the right/ down-below for a quick price.
- Crane type:_____ . (e.g., overhead crane, gantry crane, jib crane)
- Max weight to lift:_____ tons. (e.g., 2t, 5t, 10t, 20t, 50t)
- Lifting height:_____ m. (How high does the hook need to reach?
- Workshop width (span):_____ m . (Distance between the two crane rails)
- Travel distance:_____ m . (How long does the crane need to move along the runway?)
- Control type:_____. (Pendant / remote / cabin Control)
- Power supply:_____. (Local voltage & frequency – e.g., 380V, 50Hz, 3-phase)
- What will it be used for?_____ (e.g., steel fabrication, concrete products, mold handling, general manufacturing, etc.)
- Any special requirements?_____ (e.g., extreme temperature, dusty or explosive environment, special paint color, etc.)
Just leave a message via the contact form and our hoist and crane engineer will contact you with in 24working hours.
Get Your Custom Quote–Quick & Easy
Fill in what you know. Skip what you don't – we'll help.Any question will be reply with 24 working hours